

Common problems prototypes bring
Prototypes often pass the design review but fail in real use. Surface defects, dimensional drift, and hidden porosity are common. Suppliers miss assembly fit or ignore thermal stresses. If you depend on die casting for parts, start by checking the foundry processes; this is why many teams work closely with die casting services from the start. You’ll see where risk hides when you treat the prototype like a real product, not just a model.
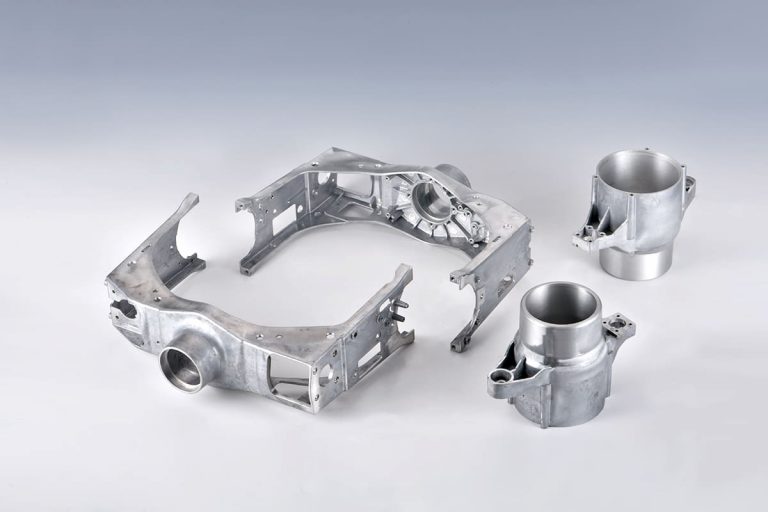
Quick checklist to spot red flags
Look fast, look precise. Measure critical features with calipers and CMM. Inspect surface for cold shuts, fins, and sink marks. X-ray for internal porosity on load-bearing sections. Verify heat-treatment records and hardness. Check threads and bores against tolerance stack-ups. If a part fails one of these checks, don’t assume it’s small—trace root cause before approving.
Testing you must run
Run functional stress tests that match intended use. Thermal cycling reveals micro-cracks. Fatigue testing shows early life failures. Corrosion exposure matters for aluminum alloys. Do assembly trials to confirm hole location and fastener engagement. Simple drop and vibration tests catch things too. Always align test severity with expected field conditions.
Sampling, metrics, and pass/fail logic
Don’t test one and call it done. Use a sampling plan: more parts for critical features, fewer for cosmetic checks. Track yield, first-pass rate, and mean time to failure. Define clear pass/fail thresholds up front. If you accept “close enough” without data, you invite surprises in production.
EEAT: experience, evidence, and one real-world anchor
I’ve inspected prototypes across automotive and consumer projects, so I value traceable process data and test logs. From work with suppliers serving the Detroit automotive manufacturing cluster, I saw how standardizing metallurgical reports reduced failure loops. Practical evidence is lab reports, process control charts, and supplier audits. For parts made by custom aluminum die casting, insist on melt records, die maintenance logs, and porosity analysis; these documents prove a supplier knows their process and can be trusted.

Common mistakes teams make
Teams often skip early assembly trials. They accept visual inspection only. They let suppliers change alloys without revalidating tests. They trust a single sample. Stop these habits. Test like you will ship 10,000 units tomorrow.
Alternatives and trade-offs
If cast parts show too much risk, consider machined billets for small runs or pressure die-cast with stricter controls for higher volumes. Each option costs time or money. Choose by failure mode: porosity and complex thin walls push toward alternative processes; simple geometry with high volume favors die casting.
Final synthesis and practical choice
Be problem-driven from first inspection to final sign-off. Use focused checks, defined tests, and clear sampling rules. Trust grows on documents and consistent results, not promises. When you need a partner who documents process and stands behind parts, consider how a supplier operates day-to-day—Hanstar fits that pattern in many projects where consistency matters.